
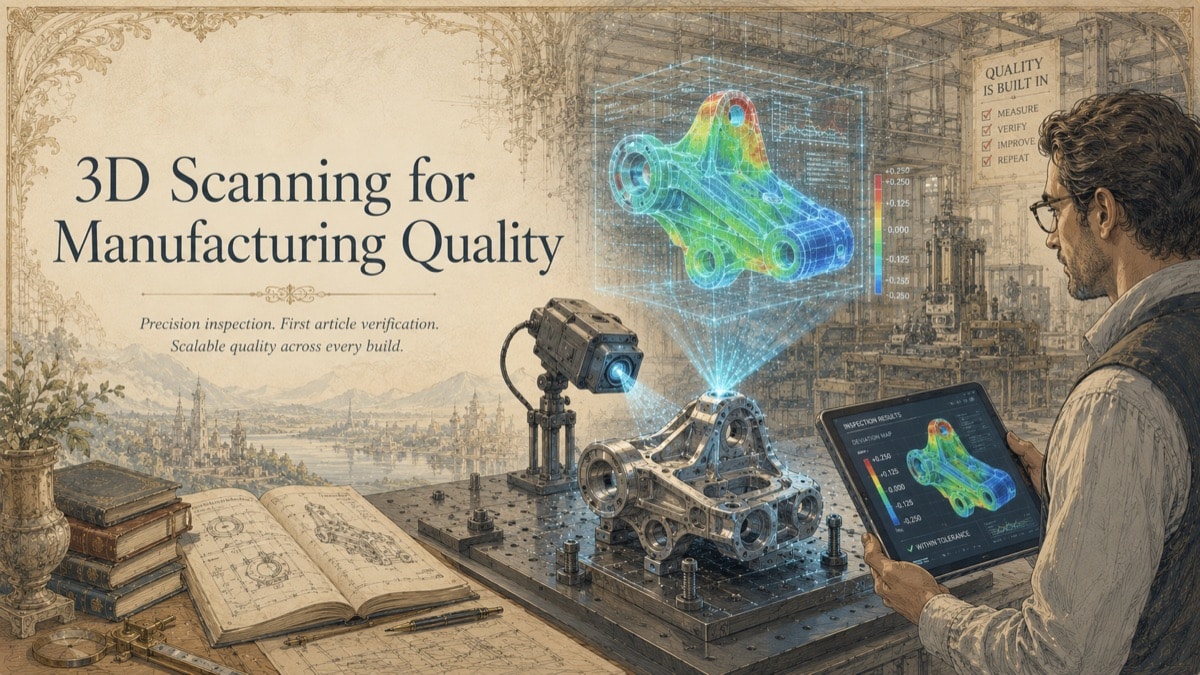
A quality team has a complex part, an approved model, and a decision to make. Traditional gauges are effective for selected features, but the team also needs to understand broad surface form, distortion, or relationships across the assembly.
3D scanning can add full-field geometric evidence for accessible surfaces. It does not automatically create a complete first article inspection, verify every GD&T characteristic, or authorize acceptance.
The method must be matched to the tolerance, feature, surface, datum strategy, quality procedure, and required decision.
Where Full-Field Geometry Helps
- Comparing accessible freeform surfaces with a controlled nominal CAD model
- Reviewing broad weldment or formed-part distortion
- Documenting tooling, fixture, mold, or die geometry over time
- Supporting first-article, incoming, in-process, or corrective-action review
- Identifying areas that need targeted contact measurement or engineering review
Scanning is strongest when many spatial relationships matter. Calipers, micrometers, hard gauges, CMMs, profilometry, NDT, material testing, and other methods remain appropriate for features or properties they measure better.
A Controlled Scan-to-Comparison Process
1. Define the inspection question
Name the part, revision, characteristic, tolerance source, decision, and authorized reviewer.
2. Select the measurement method
Confirm that the equipment, setup, environment, surface preparation, calibration status, and measurement uncertainty are suitable for the feature and tolerance.
3. Capture and disclose coverage
Record accessible surfaces and identify occlusions, low-density areas, reflections, movement, or other limitations. Unmeasured areas should never be shown as passing.
4. Align using the approved basis
Best-fit, datum-based, feature-based, and control-based alignments can produce different results. The chosen method should match the drawing or approved inspection plan.
5. Report evidence separately from disposition
Present measured values, comparison settings, coverage, deviations, and exceptions. The responsible quality, engineering, customer, or contractual authority determines acceptance, concession, rework, or rejection.
Deviation Maps Are Not Verdicts
A color map shows distance between measured data and a reference under selected settings. It does not understand functional criticality, tolerance zones, datum precedence, material condition modifiers, or whether the alignment is appropriate.
Feature results and targeted measurements may be more important than the overall color display. Reports should state units, scale, reference revision, alignment, coverage, filtering, and the source of acceptance criteria.
Standards, Accreditation, and Acceptance Boundaries
SAE AS9102 establishes requirements for aerospace first article inspection documentation. AIAG PPAP is a broader production-part approval process. A scan or deviation report may contribute dimensional evidence, but it does not by itself satisfy every requirement of either process.
Where accredited testing or calibration competence is required, the contract may reference ISO/IEC 17025 or another applicable quality framework. GDS should only claim accreditation, certification, or formal inspection authority when the specific provider, method, and scope are documented.
Building the Right Report
A useful report identifies the asset, reference revision, capture date, equipment category, method, alignment, coverage, units, tolerance source, results, exclusions, status, and responsible review path.
For production programs, repeatability also depends on fixturing, environmental control, part condition, sampling strategy, software settings, and change control. Those items should be defined before trend data is treated as comparable.
Interactive Project Readiness Check
Select the items your team has already defined. This planning aid does not determine technical acceptance or replace project scoping.
Quick Facts
Continue Reading
These guides connect this topic to the next practical decision your team may need to make.
Frequently Asked Questions
Can 3D scanning replace a CMM?
Not universally. Scanning and CMM inspection have different strengths. Critical features may require contact measurement or another qualified method based on tolerance and uncertainty.
Can GDS provide an AS9102 or PPAP package?
Scan-derived dimensional evidence may support a customer-controlled process when specifically scoped. A complete AS9102 FAI or PPAP submission requires all applicable records, approvals, and quality responsibilities - not a scan report alone.
Does green on a deviation map mean the part passes?
No. Color depends on the chosen scale, alignment, coverage, and reference. Acceptance depends on the applicable requirement and authorized review.
Can scanning verify every GD&T callout?
No. Some characteristics may be supportable with suitable data and methods; others require targeted measurement, datum simulation, access, or different equipment.
How fast can an inspection report be delivered?
Turnaround depends on part condition, complexity, quantity, required measurements, reference quality, reporting format, and review requirements. The schedule should be confirmed in the proposal.
Connect this article to the right GDS workflow
GDS can help determine whether a project should begin with 3D laser scanning, 3D modeling, reverse engineering, or consulting. The correct workflow depends on the asset, intended use, required deliverable, access, and project-specific accuracy needs.
GDS provides nationwide project coverage. Current examples from the GDS locations page include Los Angeles, San Jose, Irvine, and Houston.
Ready to Define the Right Scope?
Tell GDS about the asset, decision, available records, site or part location, and intended deliverable. GDS can help identify the appropriate capture and digital workflow.